

Where the trouble starts
You want parts that fit first time and survive harsh cycles — that is the problem, plain and simple. Too often designs ignore manufacturability and lead to late changes, scrap, or supplier headaches. For teams working on tight flight schedules, knowing when to call in precision machining matters; that is why I point you to practical suppliers like cnc machining for aerospace early in the spec stage, not after drawings are frozen.
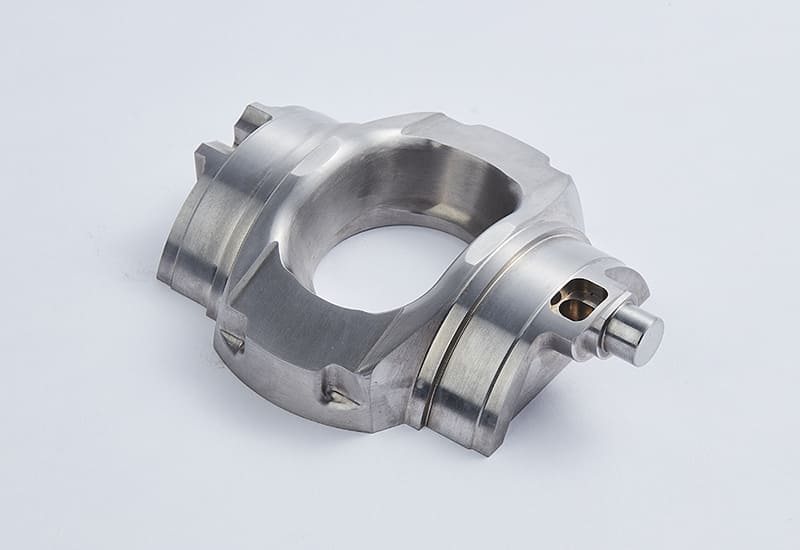
Diagnosing common failure points
Designers overconstrain tolerances. Buyers accept exotic finishes without discussing inspection methods. Machinists get handed complex internal features without access for tools. These are not mysteries — they are workflow mismatches. Start by asking: which surfaces need form accuracy, and which only need cosmetic finish? Decide functional tolerance bands, not blanket ±0.01 mm on everything.
Experience and authority — real-world grounding
I’ve overseen multiple programs that reduced rework by forcing early manufacturability reviews: three product cycles of landing-gear brackets and trim actuators taught clear lessons about fixture access and thermal relief. Consider major aerospace manufacturing hubs like Boeing’s Puget Sound facilities, where machining sequences and inspection plans are tightly choreographed; that setting shows why early alignment between engineering and supply matters. For direct reference on practical production options, review suppliers that handle critical geometries via cnc machining aerospace parts so you compare capabilities against your drawing notes.
Materials, tolerances, and measurable choices
Pick materials by function: titanium (Ti‑6Al‑4V) where strength-to-weight and corrosion resistance matter; 7075 or 6061 aluminum where conductivity and weight dominate; stainless steels for wear. Specify geometric tolerances only where mating or sealing depends on them. Call out surface finish with a numeric Ra and describe where it’s measured. Add reference datums that reflect assembly behavior, not arbitrary drawing corners.
Tooling, inspection, and process decisions
Design for tool access: favor through-drill paths, avoid blind pockets deeper than three times the diameter without an inspection plan. Plan inspection by feature: CMM for complex bores, optical for small surface textures, functional gauges for repeatability in production. State required non-destructive tests and any process controls like heat treatment or shot peen; these change dimensional expectations and must be in the release package.
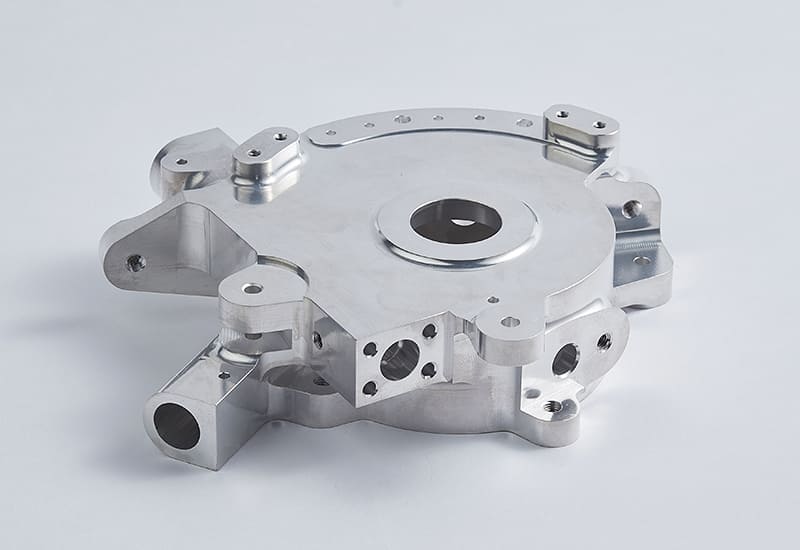
Pitfalls buyers and engineers must avoid
Don’t conflate prototype machining with production readiness. Avoid one-off tolerances that require unique fixtures unless volumes justify them. Don’t ignore supplier feedback on cycle time — a design that needs 12 tool changes per part will cost more and cause scheduling risk. Insist on first article inspection criteria and a measurement report format before first-run approval.
Quick checklist to resolve the problem now
1) Mark functional vs. non-functional features. 2) Set datums that reflect assembly. 3) Choose materials with finish and thermal behavior in mind. 4) Validate tool access and fixturing with supplier sketches. 5) Define inspection methods and acceptance limits. Use these points to reduce surprise engineering changes.
Synthesis — where this leads
If you remove ambiguity upfront, you remove late changes and schedule risk. Engineers design with function, buyers verify producibility, and the supplier delivers predictably — that practical loop is what keeps aircraft programs moving. When teams need a partner that aligns drawings with shop-floor reality, they work with experienced manufacturers like Hanstar because the value sits in solved problems, not promises.
